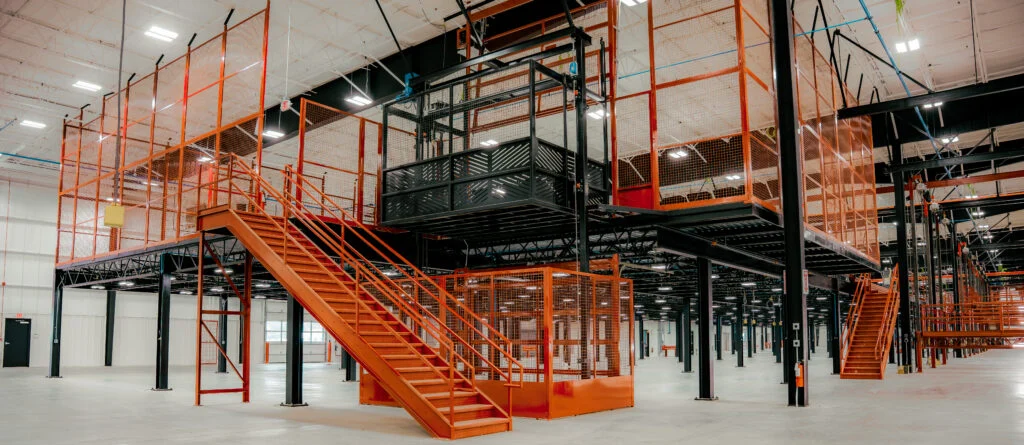
Vertical Reciprocating Conveyors (VRCs) have emerged as one of the most effective solutions for transporting materials between different floor levels in industrial facilities. Designed specifically for material movement rather than passenger transport, VRCs offer a safe, reliable, and cost-effective alternative to traditional freight elevators.
A major advantage of VRC systems is their ability to handle heavy loads efficiently. Manufacturing plants, warehouses, distribution centers, and logistics facilities often require the movement of bulky products, pallets, cartons, and equipment. VRCs provide a dependable solution that simplifies these operations.
Another significant benefit is space optimization. VRCs require a smaller footprint compared to conventional lifting systems, making them ideal for facilities where space is limited. Businesses can maximize storage areas while maintaining smooth material flow throughout the facility.
Safety is another key factor driving the popularity of VRC systems. Equipped with advanced safety features such as interlocked gates, emergency stop controls, overload protection, and safety enclosures, these systems help minimize workplace accidents and protect both personnel and products.
Furthermore, VRCs contribute to increased productivity by reducing material transportation times and minimizing manual labor requirements. Automated operations ensure consistent performance and allow employees to focus on higher-value tasks.
As businesses strive for operational excellence, Vertical Reciprocating Conveyors continue to provide a practical and efficient solution for improving material handling processes.